Industrial CNC Lathe Maintenance Checklist: Preventing Spindle Runout & Tool Wear
A practical shop floor maintenance schedule to prevent spindle radial runout, eliminate backlash on ball screws, and double the working life of your slant bed and flat bed CNC lathes.
Why Preventive Maintenance Directly Protects Your Bottom Line
A well-maintained CNC lathe will comfortably hold ±0.005 mm tolerances for over a decade. Conversely, neglecting lubrication pressure, coolant filtration, or hydraulic chuck cleanliness can degrade accuracy within 6 months, leading to premature bearing failure and costly unplanned downtime.
Here is the operational checklist recommended by Mainland CNC’s service division for all TCK and CK series turning machines.
The Daily Pre-Shift Checklist (5 Minutes)
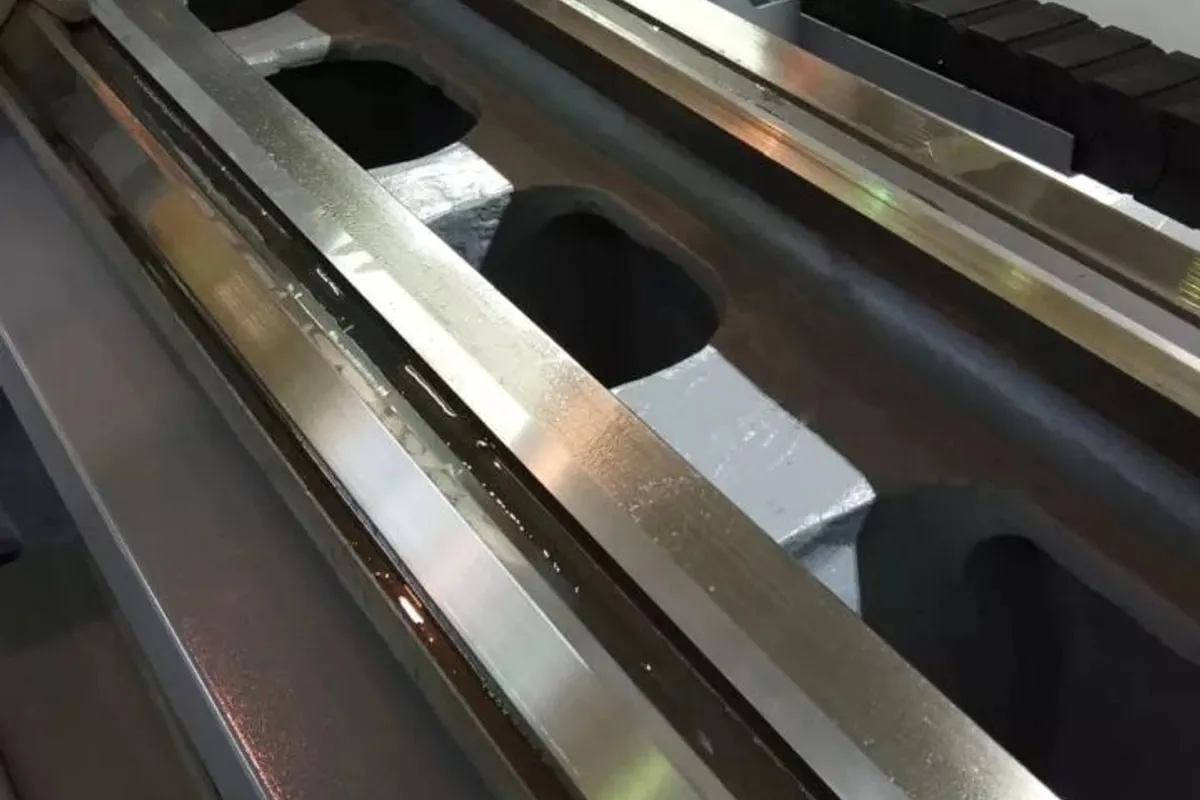
- Lubrication Oil Level: Check the central lubrication reservoir. Ensure ISO VG68 slideway oil is topped up and the manual pressure gauge reaches at least 1.5 MPa during the automatic pump cycle.
- Hydraulic System Pressure: Verify system operating pressure is maintained between 2.5 and 3.5 MPa for hydraulic chuck and tailstock clamping.
- Pneumatic Pressure: Check clean, dry compressed air supply is at a minimum of 0.6 MPa. Drain the moisture trap on the air regulator.
- Way Cover Wipers: Visually inspect telescopic way covers. Clear chips trapped between wiper lips to prevent fine swarf from scouring the guideway surface.
Weekly Maintenance Tasks (30 Minutes)
Coolant Sump & Filtration
  ├── Measure Refractometer Concentration (6% - 9% for steel, 8% - 11% for stainless)
  ├── Skim Tramp Oil from Coolant Surface (Prevents anaerobic bacterial growth)
└── Clean Filter Strainer Baskets in Chip Conveyor- Clean Chuck Jaws & Master Serrations: Disassemble chuck top jaws, brush clean the master jaw serrations with solvent, and lubricate with high-pressure molybdenum disulfide chuck grease. Lack of greasing can reduce clamping force by up to 50%!
- Inspect Spindle Radial Runout: Mount a 0.001 mm dial test indicator (DTI) on a magnetic base against the spindle nose inner taper. Rotate by hand; radial runout must not exceed 0.003 mm.
Monthly & Quarterly Checklist
| Component | Inspection Action | Specification / Threshold |
|---|---|---|
| X/Z Ball Screws | Check axial end-play using DTI while jogging axis in 0.001 mm increments | Backlash must be < 0.008 mm before electronic compensation |
| Hydraulic Oil Tank | Inspect oil clarity and temperature. Change ISO VG46 hydraulic oil every 2,000 hours | Operating temp < 55°C |
| Belt Tension | Check motor-to-spindle drive belts for glazing, cracking, and deflection | 10 mm deflection under 30 N finger force |
| Electrical Cabinet | Vacuum filter mesh on cooling fans. Check for loose terminals or moisture | Filters must be free of airborne oil mist |
| Turret Curvic Coupling | Inspect repeatability when clamping boring holders | Radial runout < 0.005 mm |
Handling Emergency Maintenance & Spare Parts
Even with pristine maintenance, normal mechanical wear requires spare parts availability. Mainland CNC maintains a comprehensive inventory of:
- Cartridge spindles and matched angular contact bearing sets
- Pre-ground C3 precision ball screws and support bearings
- Hydraulic chuck seals, rotary cylinders, and solenoid valves
- Controller backup batteries, drive modules, and handwheels
Need technical support or replacement consumables? Contact our global service desk anytime at xiuc32860@gmail.com.
Looking for the right CNC machine tool for your workpiece? Speak directly with our application engineers.
Send us your component drawings or cutting requirements. Our engineering team will simulate cycle times, recommend tooling packages, and provide factory-direct CIF pricing.